How Are Slab Gate Valves Tested for Pressure and Leakage?
A slab gate valve is often the last line of defense in pipelines that carry crude oil, natural gas, and processed products between controlled flow and a significant event. These valves are for isolating high-pressure sections for years at a time, so the buyers want to ensure that each one holds pressure and seals tightly before it is installed. The verification is carried out by a systematic test program that encompasses the valve shell, the seats, the stem seals, and the overall functioning. This paper discusses the testing of a slab gate valve for pressure and leakage, the standards and acceptance criteria that govern the work, the equipment and conditions that are crucial, and the translation of the testing results into dependable field performance.
Understanding Why Testing Matters for a Slab Gate Valve
Safety and Containment
All slab gate valves installed in an oil or gas line are expected to retain fluid at full working pressure, sometimes with sour or abrasive particles inside. Leakage may be an issue from a weak body casting, a poorly seated gate, or a damaged stem seal, which is expensive to repair and hard to predict. Pressure testing and leak testing remove such ambiguities. Prior to shipment, manufacturers test the integrity of the pressure-containing parts of the valve by pressurizing the valve to pressures far greater than usual operating pressures. That means operators get a slab gate valve and documented assurance that will protect people, equipment, and the environment from day one of operation.
Compliance With Industry Standards
Testing is not a subject for individual judgment. Standards such as API 6D for pipeline valves and API 6A for wellhead equipment control the pressure test that a slab gate valve has to pass, the duration of the test, and the maximum allowable leakage. The leakage rates and test medium for general industrial valves are specified in accompanying standards such as API 598 and ISO 5208. These agreements provide a shared language between producers and customers. Procurement teams may compare apples to apples, and inspectors can check results against a defined, published baseline when a slab gate valve is tested to a recognized standard.
Lifecycle Cost and Reliability
Testing thoroughly also saves money. A good slab gate valve that survives the most demanding factory testing is less likely to need premature repair, emergency replacement, or unplanned shutdowns. Pipeline outages are expensive, and the cost of a failure might be higher than the purchase price of several valves. Such field failure is prevented by testing that exposes casting defects, machining errors, or assembly problems on the shop floor. A well-proven slab gate valve provides the owner with more steady operation, less intervention, and a lower total cost of ownership throughout the life of a project.”
Core Pressure Testing Methods for a Slab Gate Valve
Hydrostatic Shell Test
The simplest and first test is the hydrostatic shell test. The valve is slightly open; the ends are shut up. The body is filled with water or a similar test liquid to the requisite pressure level (often 1.5 times the rated operating pressure). The pressure is maintained for a period of time in which the examiners evaluate the body, bonnet and end connections for leaks, perspiration or visible deformation. Liquid is practically incompressible, and so this process is seen as safe and reliable. Shell testing of a slab gate valve has shown that its pressure boundary can withstand stresses much beyond typical operating conditions.
Hydrostatic Seat Test
After the shell test, it’s the seats’ turn. For the seat test, the slab gate valve is closed, and pressure is supplied to one side of the gate, and the other side is monitored for leakage. The test is then run in the other way, as needed by the design. Any liquid that passes the seat during the holding period will be measured by inspectors and compared to the acceptance limit in the standard. Most designs of slab gate valve seats are either metal-to-metal or soft-insert with precision-machined surfaces. This test is to check if the gate and seats make proper contact under real pressure differentials.
Low-Pressure and High-Pressure Gas Testing
Water tests are necessary, but gas testing will discover very small leaks that water could miss. Many standards have the valve body immersed in or covered with a leak-detection solution. Supply air or nitrogen at low and high pressure. Bubbles are released as gas. Helium and a mass spectrometer may also be used to test a slab gate valve for critical service and can identify extremely tiny leaks. Due to the energy stored, gas testing is done in very safe conditions. If a slab gate valve has passed the liquid test and the gas test, the buyer may be certain the tightness is excellent.
The table below compares the main pressure test types used for a slab gate valve.
| Test Type | Typical Medium | Main Purpose | Common Pressure Level |
|---|---|---|---|
| Hydrostatic shell test | Water | Verify body and bonnet strength | About 1.5 times rated pressure |
| Hydrostatic seat test | Water | Verify gate and seat sealing | Rated pressure or standard value |
| Low-pressure gas seat test | Air or nitrogen | Detect fine leakage | Low pressure per standard |
| High-pressure gas test | Nitrogen or helium | Confirm tightness for critical service | Rated pressure per specification |
Leakage Detection and Acceptance Criteria
Seat Leakage Classes and Limits
Leakage is not pass or fail; standards establish allowed rates. For example, under API 598, soft-seated valves are anticipated to demonstrate no apparent leakage throughout the test time, but metal-seated valves may be permitted a limited rate depending on valve size. ISO 5208 divides leakages into rate levels A to G. Class A is the most stringent and does not allow visible leakage. Buyers choose the class that fits their process and safety demands when ordering a slab gate valve. Both parties will understand these classes and agree on the appropriate tightness before manufacture starts.
Stem Seal and Body Joint Inspection
Leakage may occur in areas other than the seat. During testing, inspectors assess each slab gate valve for external leakage at the stem packing, bonnet gasket, and end flange connections. Fugitive emission tests (e.g. ISO 15848) detect tiny quantities of gas that are released through the stem seal during several operational cycles. Leakage to the outside is becoming ever more significant, notably for environmental and safety considerations in gas service. A slab gate valve that minimizes internal and exterior leakage enables cleaner, safer plant operation.
Documentation and Traceability
Test results are meaningful only if documented correctly. A test report is provided for each slab gate valve, generally including the serial number, test pressures, hold periods, media, and the inspector’s confirmation. Material certifications and heat numbers are associated with the same record, so you can track any component back to its source. Many clients also see the tests themselves or hire third-party inspectors to visit the plant. Clear documentation serves as a reliable reference for the engineering, procurement, and maintenance teams for the whole life of the slab gate valve.
Equipment, Procedures, and Quality Control in the Factory
Test Benches and Instrumentation
Reliable equipment means reliable outcomes. Modern valve test benches use hydraulic clamping, calibrated pressure gauges, digital transducers, and automatic data recording. The calibration is so good that we can trust every reading. For a big slab gate valve, the bench must hold the valve securely against thousands of pounds of force while the pressure is delivered. Automated systems record the pressure curves during the hold time, which eliminates human error and makes the data easier to evaluate. Good instrumentation converts testing from a manual check to a repeatable, traceable measuring procedure.
Step-by-Step Test Procedure
It is a predetermined sequence that maintains all tests uniform. A typical technique for a slab gate valve involves the following steps:
- Clean the valve and ensure all pieces are assembled properly.
- Install the valve on the test bench and connect the test lines.
- Test and hold shell pressure for the desired period.
- Conduct seat tests in all the necessary directions.
- Gas testing and leak detection checks (where indicated)
- Drain and dry the valve. Record all findings and sign the report.
Results may be consistently compared across batches, sizes, and pressure classes by using the same techniques for each unit.
Factory Capability and Certification
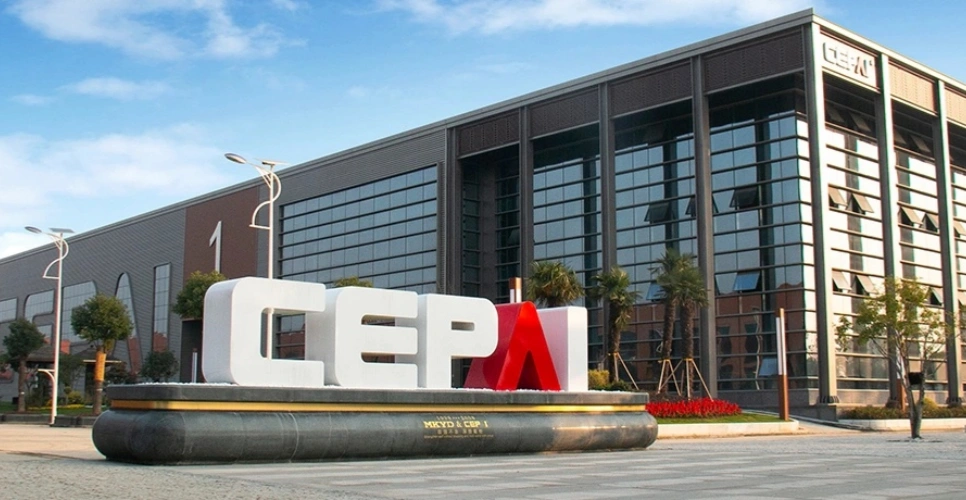
The strength of a manufacturer’s test program is the strength of the entity that is executing the program. CEPAI Group Co., LTD. was established in 2009 in Jinhu, Jiangsu Province. It features a plant of 56,000 square meters and a CNAS nationally approved laboratory. The company is API Q1, API 6A, API 6D, API 16C, API 602, ISO 9001, ISO 14001, ISO 45001, ISO 3834, ISO 17025, CE, and PR2 certified. It is also a Jiangsu smart plant and has earned the Mayor Quality Award. For the customer, this certification assures that all the slab gate valves are made and tested under a controlled and auditable system.
Turning Test Results Into Field Performance
Choosing the Right Slab Gate Valve
Buyers use test results to pick the right product. To choose the right slab gate valve for a project, engineers can look at its pressure rating, leaking class, and material grade. The valve can be used for sour gas, high-pressure crude, or coarse slurry. Ask for test results so you can compare suppliers based on facts, not promises, when making your choice. It's possible that the seller trusts the goods if they are willing to be asked about how they test them. When you take the time to look over this information, you can better match people and have fewer surprises when you commission them.
Installation and Commissioning Checks
Factory tests lay the groundwork, while inspections in the field fill in the details. Usually, after installing a slab gate valve, line pressure tests are done, the valve's smooth opening and closing is checked, and the flange joints are looked at visually for leaks. The closing surfaces are kept safe by making sure the pipes are straight, the bolts are tight, and the surfaces are clean. If you compare the data from the field to the report from the factory, you may get a good idea of whether everything is working right away. Finally, this third step connects the quality that goes into making something to the performance that happens on site.
Maintenance and Periodic Retesting
Regular upkeep is needed for a long working life. Usually, each slab gate valve would be set up to be inspected by the plant more than once. This includes lubricating the stem, checking the packing, and testing for seat leakage during planned shutdowns. Before a valve is put back into service after being rebuilt or fixed, it is tested again. Every recorded test builds a history that helps operators figure out when maintenance is going to be needed. For tough oil, gas, industrial, and power uses, a slab gate valve can be safely closed for many years with regular testing and upkeep.
The table below shows how testing supports each stage of a valve’s life.
| Stage | Key Activity | Value to the Owner |
|---|---|---|
| Manufacturing | Shell, seat, and gas tests | Proven pressure integrity |
| Selection | Review of reports and leakage class | Better product matching |
| Commissioning | Line pressure and operation checks | Confirmed site performance |
| Operation | Periodic inspection and retesting | Longer, safer service life |
Conclusion
Testing is what makes a well-built slab gate valve a reliable piece of pipeline equipment. Tests of the hydrostatic shell show that the body can handle pressures that are much higher than what is normally used. Seat tests proved that the shutdown was tight. Tests for gas leakage show that the leakage classes give everyone a clear way to get approved. Test benches that have been calibrated, set standards, and written test records make sure that the results can be trusted and tracked. That trust was built every day through field checks and regular retests. If you choose a vendor with well-known credentials and the ability to do lab tests in-house, you can be sure that the slab gate valve you buy is backed by real evidence. Look over the test results, make sure you ask the right questions, and work with a manufacturer that will back you up.
FAQ
1. What is the purpose of a hydrostatic shell test on a slab gate valve?
It confirms that the body, bonnet, and end connections can safely withstand pressure well above the rated working level.
2. How is seat leakage checked on a slab gate valve?
The valve is closed, pressure is applied to one side, and the opposite side is monitored for leakage during a set holding period.
3. Which standards govern slab gate valve testing?
API 6D, API 6A, API 598, and ISO 5208 are commonly used to define test methods and leakage limits.
4. Why is gas testing performed in addition to liquid testing?
Gas can reveal very fine leaks that water may not show, giving extra confidence in sealing performance.
5. What documents come with a tested slab gate valve?
A test report with serial number, pressures, hold times, and inspector approval, together with material certificates.
Request Tested Slab Gate Valve Solutions From CEPAI Today
A valve is only as dependable as the testing behind it. CEPAI Group Co., LTD. combines certified quality systems, a CNAS-recognized laboratory, and a smart factory to deliver slab gate valves that are tested thoroughly and documented clearly. Whether your project involves oil and gas pipelines, petrochemical plants, or power facilities, our engineers can help you choose the right size, pressure class, and leakage standard for your needs. Send us your requirements, and we will prepare a professional proposal with full test documentation. Contact our team at sales@cepai.com today and let us help you build safer, more reliable pipeline systems.
Get professional pre-sales technical consultation and valve selection services, customized solution services.
About CEPAI
Popular Blogs